
Home / Overmolding service
Overmolding service
Bond soft rubber directly onto hard plastic parts. We deliver comfortable grips and waterproof seals that never peel off, crack, or leak.
- 50+ Validated Rigid-Soft Pairings
- Zero Delamination & Flash-Free Edges
- Shore A 30 to D 80 Custom Grips
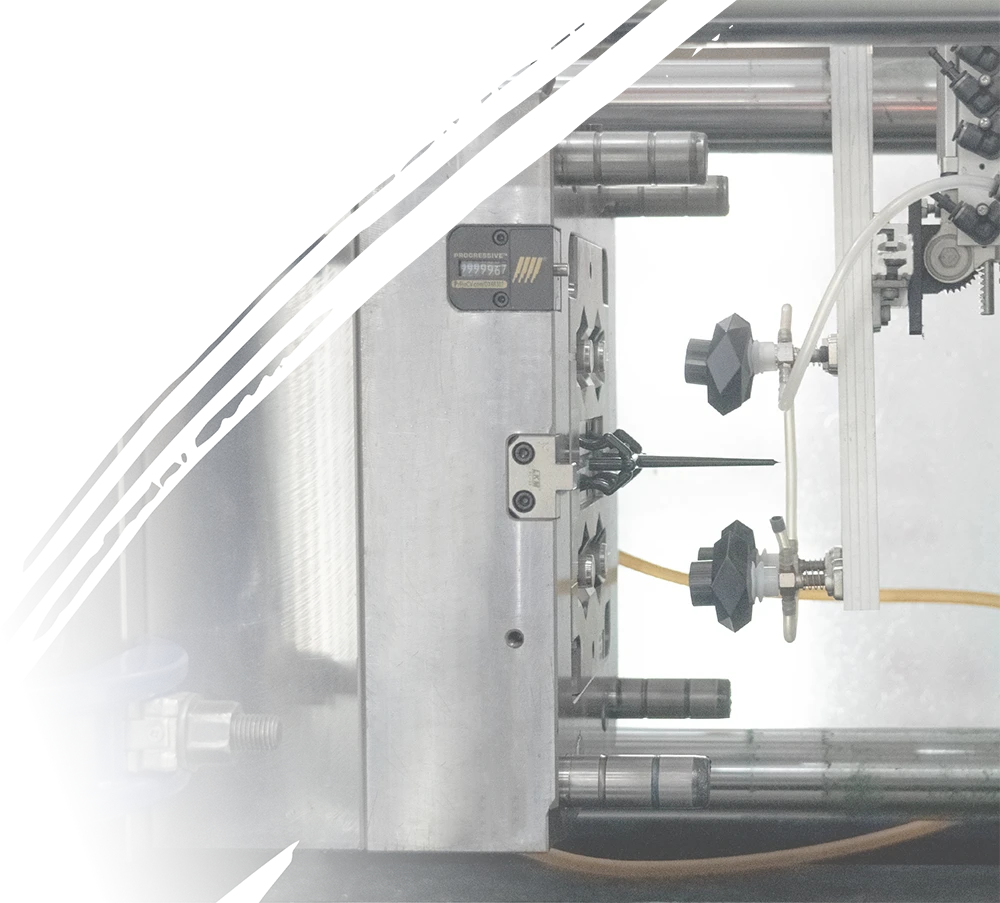
Compatible Overmolding Applications
In product design, you often need to improve grip, add waterproofing, or enhance appearance by wrapping a soft material (like TPE, TPU, or silicone) around a rigid plastic base. This is exactly what overmolding achieves. You see this everyday in tool handles, toothbrush grips, and rugged phone cases.
Unlike manual assembly or gluing, overmolding is a multi-step injection process that permanently bonds the second material directly onto the hard plastic substrate. For your projects, this means instantly adding ergonomic or protective features with no assembly gaps and zero peeling.
Ergonomic Grips & Tactile Surfaces
Adds soft, non-slip TPE or TPU to hard plastic parts. Commonly used for power tool handles, wearables, and control knobs.
Integrated Seals & Gaskets
Bonds rubber directly to housings to replace separate O-rings. Creates reliable IP67/IP68 waterproof and dustproof seals.
Impact Protection & Insulation
Uses thick rubber layers to absorb shock or provide electrical insulation. Ideal for rugged device corners and cable strain reliefs.(
Two-Tone Aesthetics & Structure
Combines different colors or materials in one part to reduce assembly. Used for brand logos, cosmetic finishes, and soft hinges.


Case Study: Resolving Shrinkage in Thick-Walled Parts
Thick plastic components, such as cosmetic caps, often develop sink marks due to uneven cooling. In this video, our Engineering Director explains how splitting a thick section into a two-step overmolding process eliminates surface distortion while maintaining the required structural thickness.
Overmolding Equipment & Specifications At First Mold
Two-step overmolding runs on standard injection molding machines, meaning the true quality of the part is determined by the mold tooling. To machine exact shut-off surfaces and prevent liquid rubber from flashing, we build our molds using industry-leading equipment, including Haas 5-axis CNCs, GF+ high-precision CNCs, and Makino EDMs. The specifications below outline our production capabilities and key design parameters.
| Specificatie | Vermogen | Specificatie | Vermogen |
|---|---|---|---|
| Elastomer Hardness | Shore A 30 – Shore D 80 | Optimal Overmold Thickness | 1.5 – 2.5 mm (for ideal tactile feel); feasible down to 1.0 mm |
| Min. Substrate Thickness | ≥ 1.5 mm (general guide to withstand injection pressure) | Recommended Draft Angle | 1.0° – 2.0° standard; add 0.5° – 1.0° for textured surfaces |
| Bindingsmethoden | Chemical Adhesion & Mechanical Interlocking | Adhesion Testing Standard | ASTM D903 (Peel) / ASTM D3359 (Cross-Hatch) |
| Parts Standard Tolerance | ±0,1 mm (±0,004″) | Shut-off Precision (No Flash) | ±0,05 mm (±0,002″) |
| Custom Color Matching | Pantone, RAL, Masterbatch Compounding | Materiaalconformiteit | RoHS, REACH, FDA Class VI, Biocompatible |


Materiaalcombinaties voor overspuittechnologie
Handling 2+ new overmolding production commissions every month, First Mold’s engineering team has mastered the practical application of diverse resins and elastomers. We know exactly how to achieve a permanent, glue-free bond and prevent delamination.
| Soft Overmold | Excellent Bond | Good Bond | Poor Bond | Toepassingsvoorbeelden |
|---|---|---|---|---|
| TPE | PP | ABS, PC, PS | POM, Nylon | Automotive anti-rattle overmolds; strain-relief boots; diagnostic equipment grips |
| TPU | ABS, PC, PC/ABS | Nylon (PA) | PP, PE | Valve spool encapsulation; robotic cable joints; rugged sensor housings |
| TPV | PP | Nylon (special grade) | ABS, PC | Under-hood duct seals; EV charging weatherseals; outdoor equipment gaskets |
| TPR | PS, HIPS | PP | PC, Nylon | Precision instrument isolation pads; soft/soft suction cups; anti-vibration mounts |
| Biobased TPE | PLA, PBAT | PP | – | Diagnostic device housings; personal-care grips; compostable closures |
Why Partner with First Mold for Overmolding?
Ask yourself about your current supplier: Are their molds built in-house or outsourced? What is their aging degradation data for peel strength? When production defects arise, do they solve the root cause, or just point fingers?
Overmolding is an unforgiving process. Here is how First Mold ensures absolute accountability, verifiable quality, and the lowest total cost of ownership.
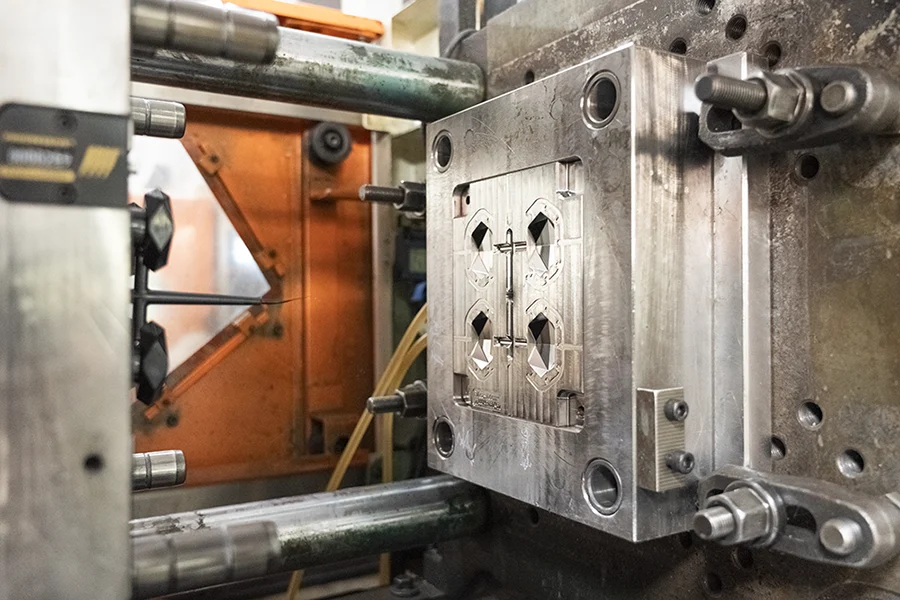
Unified Tooling & Molding Team
Whether an overmolded bond holds and whether the shut-off stays clean are about 80% decided during mold design. Because our tooling makers and molding engineers work together under one roof, no one points fingers. You never have to act as the go-between for different vendors—if a problem comes up, we find the root cause and fix it ourselves.
Data-Backed Precision & Bonding
We measure adhesion and precision—and prove the numbers. Our parts consistently achieve 180° peel strengths of 1.5–3.0 N/mm (and 4.5 N/mm or higher with plasma activation). We hold flash at critical shut-offs to ≤0.05 mm, with parting line clearances under 0.01 mm, so we can guarantee zero delamination in 72-hour salt spray tests.
Deep DFM Intervention
Lorem ipsum dolor sit amet, consectetur adipiscing elit. Ut elit tellus, luctus nec ullamcorper mattis, pulvinar dapibus leo.
Predictive Warpage Compensation
Overspuiten vs. Tussenvoegsel Vs. Tweekleurig vormen
Bij overspuiten wordt een materiaal op een bestaand substraat (zoals hard plastic of metaal) gespoten. Dit proces wordt in afzonderlijke stappen uitgevoerd om een beschermende of functionele laag te vormen. Bij insert molding worden de inserts, zoals metalen of elektronische componenten, eerst in de spuitgietmatrijs geplaatst. Daarna wordt kunststof geïnjecteerd om de inzetstukken vast te zetten en te integreren. Bij two-shot molding wordt een roterende matrijs gebruikt om twee verschillende materialen in dezelfde cyclus te injecteren.
| Afmeting | Overspuiten | Tussenvoegsel Vormen | Twee-kleuren lijstwerk |
|---|---|---|---|
| Processtappen | Injectie in twee stappen: Harde kern → Zachte overmold | Pre-insert plaatsing → Single-shot inkapseling | Injectie met twee schoten (roterende/schuivende matrijs) |
| Materiaalcombinatie | Zacht-hard verlijmen (bijv. PP+TPE) | Kunststof + metaal/insert (bijv. PA66+koper) | Tweekleurige kunststoffen (bijv. ABS+PC) |
| Vereisten voor apparatuur | Standaardmachine + compatibele matrijs | Standaardmachine + robot/handmatige plaatsing van inzetstukken | Speciale tweekleurenmachine + roterende matrijs (±0,02 mm) |
| Materiële interactie | Chemische binding (thermodynamische compatibiliteit) | Mechanische vergrendeling (geen chemische binding) | Fysieke gelaagdheid (smeltpuntsynchronisatie) |
| Structureel verschil | Gelaagde inkapseling (functionele integratie) | Kern invoegen (composiet versterking) | Naadloze gelaagdheid (esthetische fusie) |
| Schimmelkosten | $$ | $ | $$$ |
| Productiecyclus | 30-60 sec (afkoelen tussen lagen vereist) | 45-90 sec (handmatig inbrengen) | 20-40 sec (automatische dubbele opname) |
| Typische producten | Handgrepen van gereedschap, medische instrumenten | Automotive connectoren, medische elektroden | Tweekleurige achterlichten, doorschijnende toetsen op toetsenbord |
 NL
 EN
 ES
 FR
 DE
 IT
 PT
 PL
 AR
 JA
 KO
 ZH