
ホーム / オーバーモールドサービス
オーバーモールドサービス
Bond soft rubber directly onto hard plastic parts. We deliver comfortable grips and waterproof seals that never peel off, crack, or leak.
- 50+ Validated Rigid-Soft Pairings
- Zero Delamination & Flash-Free Edges
- Shore A 30 to D 80 Custom Grips
Compatible Overmolding Applications
In product design, you often need to improve grip, add waterproofing, or enhance appearance by wrapping a soft material (like TPE, TPU, or silicone) around a rigid plastic base. This is exactly what overmolding achieves. You see this everyday in tool handles, toothbrush grips, and rugged phone cases.
Unlike manual assembly or gluing, overmolding is a multi-step injection process that permanently bonds the second material directly onto the hard plastic substrate. For your projects, this means instantly adding ergonomic or protective features with no assembly gaps and zero peeling.
Ergonomic Grips & Tactile Surfaces
Adds soft, non-slip TPE or TPU to hard plastic parts. Commonly used for power tool handles, wearables, and control knobs.
Integrated Seals & Gaskets
Bonds rubber directly to housings to replace separate O-rings. Creates reliable IP67/IP68 waterproof and dustproof seals.
Impact Protection & Insulation
Uses thick rubber layers to absorb shock or provide electrical insulation. Ideal for rugged device corners and cable strain reliefs.(
Two-Tone Aesthetics & Structure
Combines different colors or materials in one part to reduce assembly. Used for brand logos, cosmetic finishes, and soft hinges.


Case Study: Resolving Shrinkage in Thick-Walled Parts
Thick plastic components, such as cosmetic caps, often develop sink marks due to uneven cooling. In this video, our Engineering Director explains how splitting a thick section into a two-step overmolding process eliminates surface distortion while maintaining the required structural thickness.
Overmolding Equipment & Specifications At First Mold
Two-step overmolding runs on standard injection molding machines, meaning the true quality of the part is determined by the mold tooling. To machine exact shut-off surfaces and prevent liquid rubber from flashing, we build our molds using industry-leading equipment, including Haas 5-axis CNCs, GF+ high-precision CNCs, and Makino EDMs. The specifications below outline our production capabilities and key design parameters.
| 仕様 | 能力 | 仕様 | 能力 |
|---|---|---|---|
| Elastomer Hardness | Shore A 30 – Shore D 80 | Optimal Overmold Thickness | 1.5 – 2.5 mm (for ideal tactile feel); feasible down to 1.0 mm |
| Min. Substrate Thickness | ≥ 1.5 mm (general guide to withstand injection pressure) | Recommended Draft Angle | 1.0° – 2.0° standard; add 0.5° – 1.0° for textured surfaces |
| 接着方法 | Chemical Adhesion & Mechanical Interlocking | Adhesion Testing Standard | ASTM D903 (Peel) / ASTM D3359 (Cross-Hatch) |
| Parts Standard Tolerance | ±0.1mm(±0.004インチ) | Shut-off Precision (No Flash) | ±0.05mm (±0.002″) |
| Custom Color Matching | Pantone, RAL, Masterbatch Compounding | 材料適合性 | RoHS, REACH, FDA Class VI, Biocompatible |


オーバーモールディング技術における素材の組み合わせ
Handling 2+ new overmolding production commissions every month, First Mold’s engineering team has mastered the practical application of diverse resins and elastomers. We know exactly how to achieve a permanent, glue-free bond and prevent delamination.
| Soft Overmold | Excellent Bond | Good Bond | Poor Bond | 適用例 |
|---|---|---|---|---|
| ティーピーイー | PP | ABS, PC, PS | POM, Nylon | Automotive anti-rattle overmolds; strain-relief boots; diagnostic equipment grips |
| TPU | ABS, PC, PC/ABS | ナイロン(PA) | PP, PE | Valve spool encapsulation; robotic cable joints; rugged sensor housings |
| ティーピーブイ | PP | Nylon (special grade) | ABS, PC | Under-hood duct seals; EV charging weatherseals; outdoor equipment gaskets |
| ティーピーアール | PS, HIPS | PP | PC, Nylon | Precision instrument isolation pads; soft/soft suction cups; anti-vibration mounts |
| バイオベースTPE | PLA, PBAT | PP | – | Diagnostic device housings; personal-care grips; compostable closures |
Why Partner with First Mold for Overmolding?
Ask yourself about your current supplier: Are their molds built in-house or outsourced? What is their aging degradation data for peel strength? When production defects arise, do they solve the root cause, or just point fingers?
Overmolding is an unforgiving process. Here is how First Mold ensures absolute accountability, verifiable quality, and the lowest total cost of ownership.
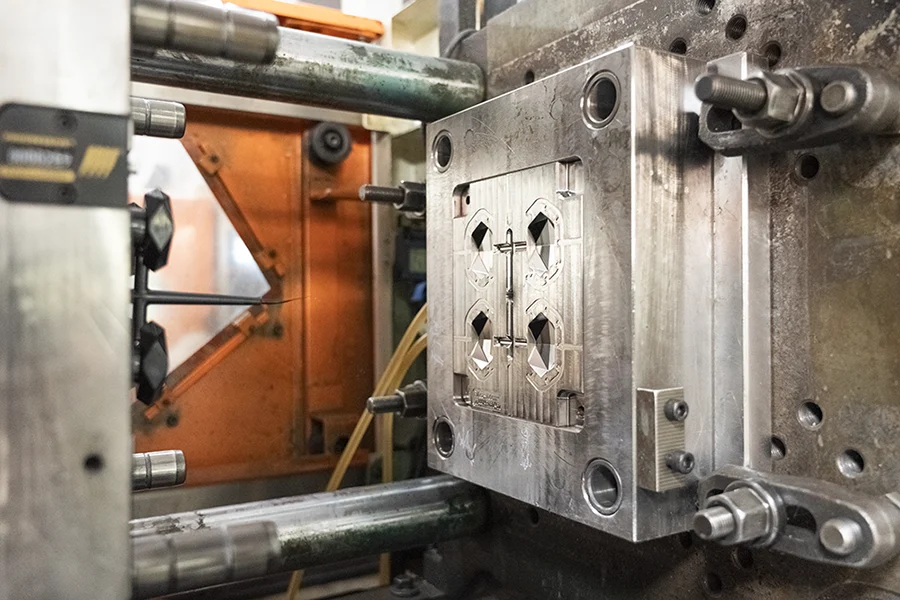
Unified Tooling & Molding Team
Whether an overmolded bond holds and whether the shut-off stays clean are about 80% decided during mold design. Because our tooling makers and molding engineers work together under one roof, no one points fingers. You never have to act as the go-between for different vendors—if a problem comes up, we find the root cause and fix it ourselves.
Data-Backed Precision & Bonding
We measure adhesion and precision—and prove the numbers. Our parts consistently achieve 180° peel strengths of 1.5–3.0 N/mm (and 4.5 N/mm or higher with plasma activation). We hold flash at critical shut-offs to ≤0.05 mm, with parting line clearances under 0.01 mm, so we can guarantee zero delamination in 72-hour salt spray tests.
Deep DFM Intervention
吾輩は猫である。名前はまだない。どこで生れたか頓と見当がつかぬ。何でも薄暗いじめじめした所でニャーニャー泣いていた事だけは記憶している。
Predictive Warpage Compensation
オーバーモールディング対インサート成形インサート成形二色成形
オーバーモールドとは、既存の基材(硬質プラスチックや金属など)の上に、ある材料を注入することである。この工程は、保護層や機能層を形成するために別々の工程で行われます。インサート成形では、まず金属や電子部品などのインサートを射出成形金型に入れます。その後、プラスチックを射出してインサートを固定し、一体化させる。ツーショット成形では、回転する金型を使って、同じサイクルで2つの異なる材料を射出する。
| 寸法 | オーバーモールディング | インサート成形 | 2色成形 |
|---|---|---|---|
| プロセスステップ | 2段階のインジェクション:ハードコア → ソフトオーバーモールド | 事前挿入 → シングルショット封止 | デュアルショット射出(回転/スライド金型) |
| 素材の組み合わせ | ソフト-ハード接合(PP+TPEなど) | プラスチック+金属/インサート(例:PA66+銅) | デュアルカラー・プラスチック(ABS+PCなど) |
| 機材要件 | 標準機+互換金型 | 標準機+ロボット/手動インサート配置 | 専用2色機+回転金型(±0.02mm) |
| 素材の相互作用 | 化学結合(熱力学的互換性) | 機械的ロック(化学結合なし) | 物理的レイヤリング(融点同期化) |
| 構造の違い | レイヤーカプセル化(機能統合) | インサートコア(複合補強材) | シームレスなレイヤリング(美的融合) |
| 金型費用 | $$ | $ | $$$ |
| 生産サイクル | 30~60秒(レイヤーとレイヤーの間に冷却が必要) | 45~90秒(手動挿入) | 20~40秒(自動デュアルショット) |
| 代表的な製品 | 工具ハンドル、医療器具 | 自動車用コネクタ、医療用電極 | デュアルカラーテールライト、半透明のキーボードキー |
 JA
 EN
 ES
 FR
 DE
 IT
 PT
 NL
 PL
 AR
 KO
 ZH