Custom plastic parts manufactured to your exact CAD specifications. Engineered with strict process controls to eliminate warpage, sink marks, and dimensional variations.
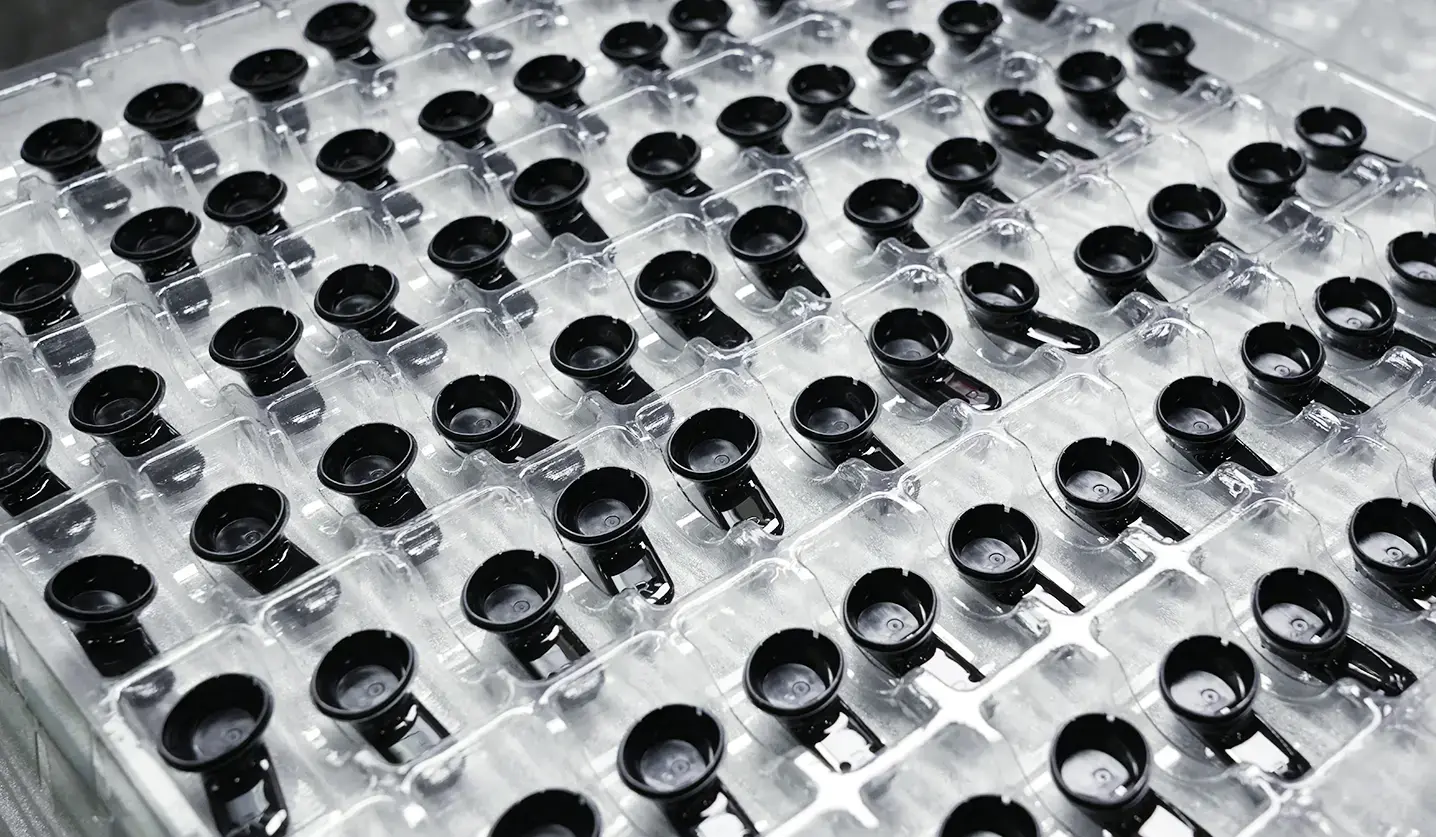
We mold over 100 commercial and engineering-grade resins every year. Our injection molding process accommodates custom Pantone color matching, UV stabilizers, and up to 50% glass fiber (GF) reinforcement for enhanced strength.
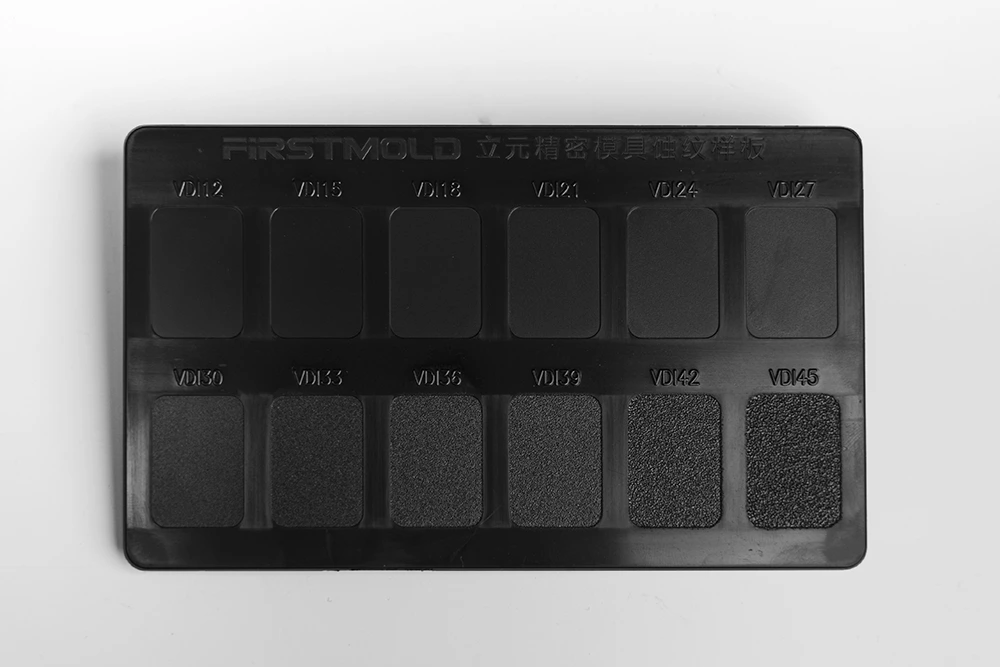
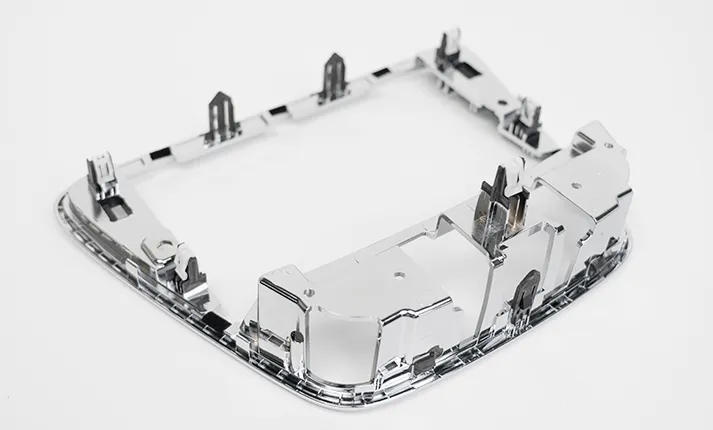
The mold shapes the part; the finish defines how it looks, feels, and performs. From in-mold SPI/VDI textures to advanced post-molding operations, we provide end-to-end finishing services to turn raw molded parts into production-ready components.
인몰드 마감 처리
표준
완주 부문
표면 거칠기 Ra (µm)
SPI A1 – A3
다이아몬드 버프 / 고광택
0.012 – 0.10
SPI B1 – B3
사포 / 반광택
0.05 – 0.32
SPI C1 – C3
스톤 마감 / 매끄러운 무광
0.35 – 0.7
SPI D1 – D3
미디어 블래스트 / 질감 처리
0.80 – 18.0
VDI 3400 (12‑45)
EDM / 방전 가공 질감
0.40 – 18.0
부품에 적용할 정확한 외관 또는 기능적 마감 처리를 결정하는 데 도움이 필요하신가요? 언제든지 직접 당사의 DFM 엔지니어에게 문의하세요 프로젝트별 권장 사항을 확인하려면.
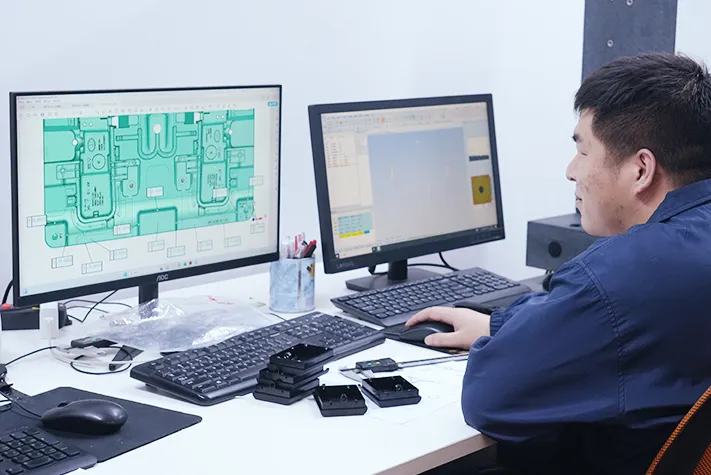
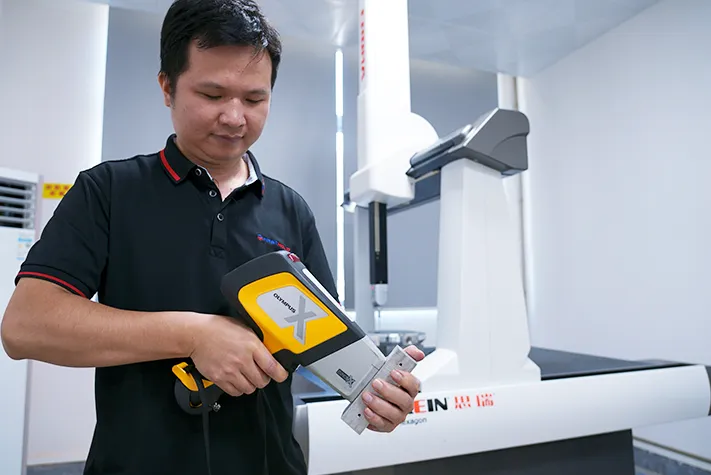
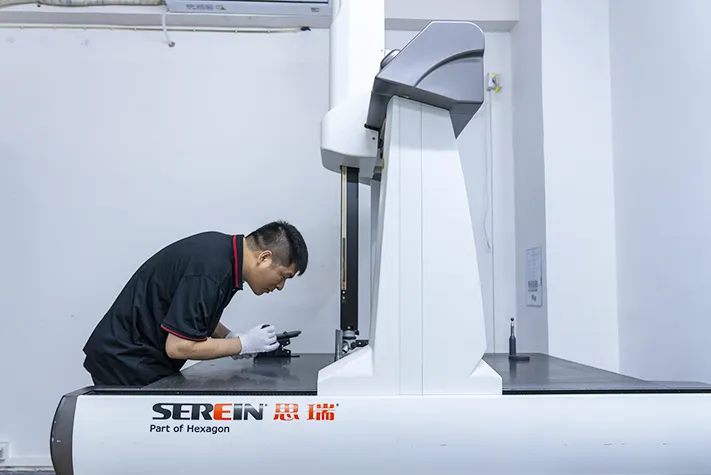
We rely on metrology and statistical process control (SPC), not guesswork. First Mold inspects and corrects critical parameters across multiple production stages.
QA Stage
당사의 방법 및 장비
주요 점검 사항
1. 사전 제작
DFM 검토 및 몰드 플로우 해석
초안 각도, 벽 두께 균일도, 게이트 위치, 용접선, 함몰, 뒤틀림 예측, 수축률, 언더컷, 냉각 채널 배치, 배기 전략.
2. 공구 및 설비
First-article Inspection (FAI) & T1 Sampling
치수 정확도, 3D CAD 일치도, 재료 검증, 표면 마감 품질, 조립 적합성, 플래시 감지, 분할선 불일치, 사출 불량, 이젝터 핀 자국.
3. 공정 중 및 최종
CMM & 2d Vision Measurement
중요 공차, 복잡한 형상, GD&T(기하학적 치수 및 공차), 평탄도, 동심도, 구멍 직경, 프로파일 편차, 실제 위치, 수직도.
4. 시스템 및 규정 준수
ISO 인증 프로토콜 및 추적성
자재 추적성, 배치 간 일관성, 표준 운영 절차(SOP) 이행, 품질 관리 보고서, 수지 분석 증명서(COA), 결함 최소화, 금형 유지보수 기록부.
Industry-Specific Molding Solutions & Case Studies
A closer look at how we solve complex manufacturing challenges across automotive, medical, consumer electronics, and industrial sectors using tailored resins and strict process controls.
Our Plastic Injection Molding Workflow at First Mold
We don’t treat your CAD files as a black box. At First Mold, our plastic injection molding process is completely transparent. Here is the exact step-by-step roadmap.
01
Submit CAD for Engineering Review
Upload your 3D models (STEP/IGES/X_T). Our engineers analyze your geometry and provide an itemized plastic injection molding quote and initial feasibility feedback within 24 hours.
02
DFM Approval & Mold Fabrication
Review our comprehensive DFM report detailing draft angles, shrink rates, and gating strategies. Upon your sign-off, we immediately begin CNC machining and cutting steel for your custom mold.
03
T1 Sampling & FAI Verification
We shoot the first physical plastics from your mold. You receive these T1 off-tool samples alongside a complete First Article Inspection (FAI) dimensional report for your engineering validation.
04
Mass Production & Global Logistics
Once you approve the T1 samples, we lock in the molding parameters for full-scale production. First Mold manages strict SPC quality control, packaging, and direct global shipping to your facility.
Recommended Structural Design Guidelines for Injection Molding
Our engineers highly recommend applying these proven structural parameters to your CAD models to avoid costly mold modifications and achieve flawless parts on the first shot.
Apply 0.5°–2° draft on vertical walls. Make the cavity draft 0.5° larger than the core to keep the part on the core during ejection.
Locate parting lines on the part's maximum contour. Avoid high-gloss or critical assembly surfaces to minimize visible flashing.
Design text and logos as raised (embossed). Machining recessed text into the mold steel is significantly easier and cheaper than machining raised letters.
Add a 0.2–1.0mm cosmetic groove (reveal) at mating lines to seamlessly hide inevitable molding tolerances and mismatch.
Design mating lips with 0.8–2.5mm depth and 0.1mm side clearance. Keep vertical top and bottom faces at zero gap for a stable fit.
For reliable assembly, use 1.0–1.5mm cantilever thickness, length under 8x the thickness, and 0.3–0.5mm hook depth.
Plastic Injection Molding FAQ
플라스틱 사출 성형의 최소 주문 수량(MOQ)은 얼마인가요?
최소 주문 수량(MOQ) 제한이 없습니다. First Mold의 신속 금형 제작 서비스는 소량 시험 생산을 지원합니다. 당사에서 금형만 구매하시는 경우에도 소량의 사출 성형 부품을 무료로 제공해 드립니다.
제 CAD 파일을 보시기 전에 비밀유지계약서(NDA)에 서명해 주실 수 있나요?
물론입니다. 고객님께서 직접 준비하신 비밀유지약정서(NDA) 양식을 보내주셔도 되고, 당사의 표준 양식을 사용해도 됩니다. 어느 쪽이든 기꺼이 서명하고 날인해 드리겠습니다. 계약이 완전히 체결된 후에 CAD 도면을 당사로 전달해 주시면 됩니다.
전액 결제 후에는 금형의 소유권은 누구에게 있나요?
최종 대금 결제가 완료되면 금형 전체와 모든 소유권은 귀하에게 귀속됩니다. 일반적으로 당사는 귀하를 대신하여 금형을 보관합니다. 귀하는 당사와 함께 생산을 계속하거나, 언제든지 당사에 요청하여 금형을 다른 시설로 배송받을 수 있습니다.
금형 제작과 양산 시 각각 어떤 결제 조건이 적용되나요?
금형 비용의 경우, 일반적으로 계약금 + 진행 단계별 대금 + 잔금 지급 방식을 적용합니다. 양산 단계에서는 월별 결제 조건(예: 30일/60일 순결제)을 제공합니다. 구체적인 비율은 귀사의 신용 등급과 주문 금액에 따라 협의 가능합니다.
T1 샘플 제공 후 디자인 변경 사항은 어떻게 처리해야 할까요?
경우에 따라 T1 샘플 제작 후에도 설계 변경을 수용할 수 있습니다. 다만, 엔지니어링 변경 시 금형 수정 비용과 추가 시제품 제작 비용이 발생합니다. 귀사의 서명된 승인서를 접수하는 대로 수정 작업을 진행한 후, 업데이트된 T2 샘플을 재제출해 드리겠습니다. 소요 기간은 변경 사항의 구체적인 범위에 따라 달라집니다.
생산 과정에서 곰팡이 관리 서비스를 무료로 제공해 주시나요?
네 – 해당 금형이 당사 공장에서 양산 중인 한, 모든 유지보수 및 수리 비용은 추가 비용 없이 당사에서 전액 부담합니다.
부품이 공차 범위를 충족하지 못하면 어떻게 되나요?
특정 로트의 제품이 확인된 치수 공차 기준을 충족하지 못할 경우, 당사는 해당 로트에 대해 무상 교체 부품을 제공해 드리겠습니다. 동시에, 재발 방지를 위해 근본 원인을 신속히 조사하고 시정 조치를 시행하겠습니다.
제가 가지고 있는 플라스틱 수지를 사용해도 될까요?
당사는 위탁 원자재(고객이 공급하는 수지)를 접수하고 있습니다. 또한 귀사가 지정한 공급업체로부터 원자재를 구매할 수도 있습니다. 다만, 귀사가 공급한 원자재로 인해 성형 결함이 발생할 경우, 당사는 해당 원자재 자체로 인한 품질 문제에 대해서는 책임을 지지 않음을 유의해 주시기 바랍니다.
팬톤/RAL 색상 일치를 어떻게 보장하나요?
당사는 독일에서 수입한 분광광도계를 사용하며, 국제 CIE LAB 색 공간 표준을 준수합니다. 당사는 각 출하 배치의 색차(ΔE)가 1.0 이하임을 보장하며, 이는 육안으로는 사실상 식별할 수 없는 수준입니다. 각 생산 공정 시작 전, 당사의 품질 검사 담당자가 첫 번째 제품에 대한 색상 검사를 실시하여 표준 범위 내에서 배치 간 일관된 색상 일치를 보장합니다.










 KO
 EN
 ES
 FR
 DE
 IT
 PT
 NL
 PL
 AR
 JA
 ZH