الصفحة الرئيسية / خدمة قولبة حقن البلاستيك بالحقن
خدمات القولبة بالحقن البلاستيكية عالية الدقة
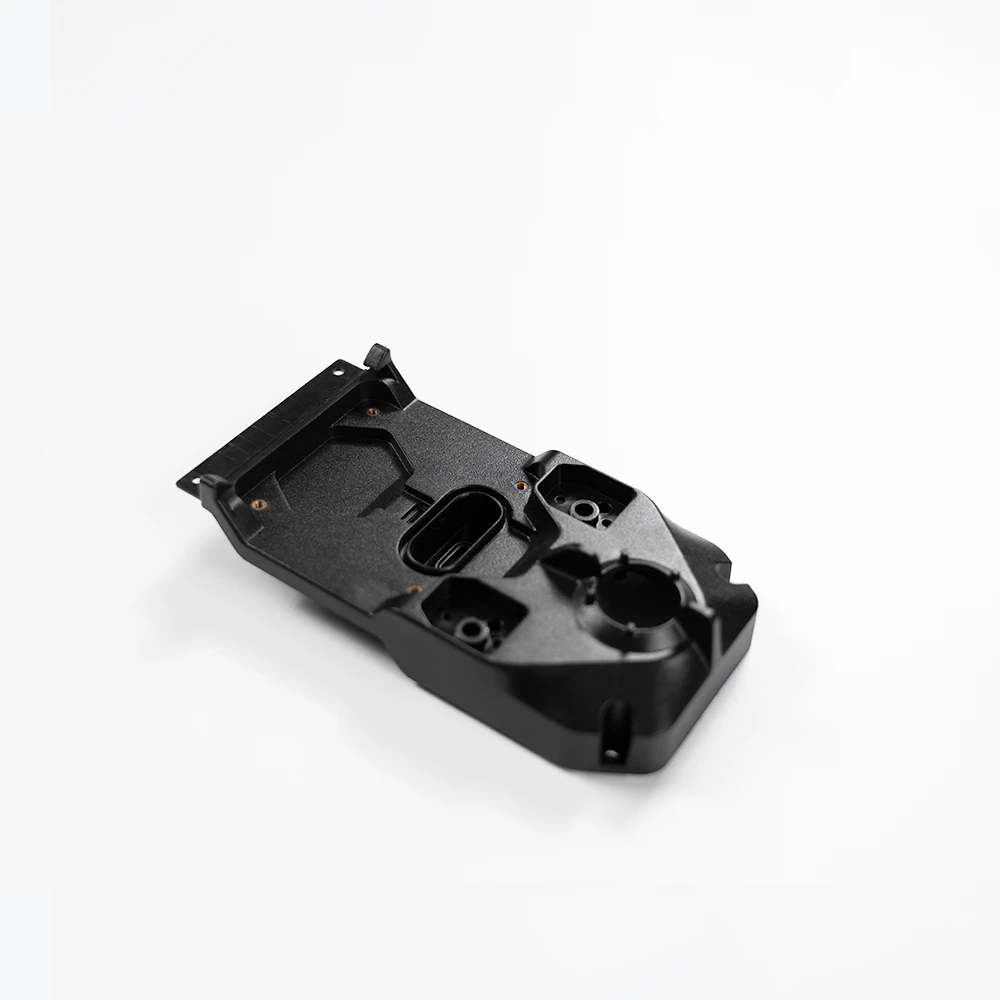
Custom plastic parts manufactured to your exact CAD specifications. Engineered with strict process controls to eliminate warpage, sink marks, and dimensional variations.
- T1 tryout samples ready in as fast as 7-15 days
- Plastic parts tolerance: ±0.05mm (±0.002")
- Comprehensive FAI Reports
القدرات الهندسية
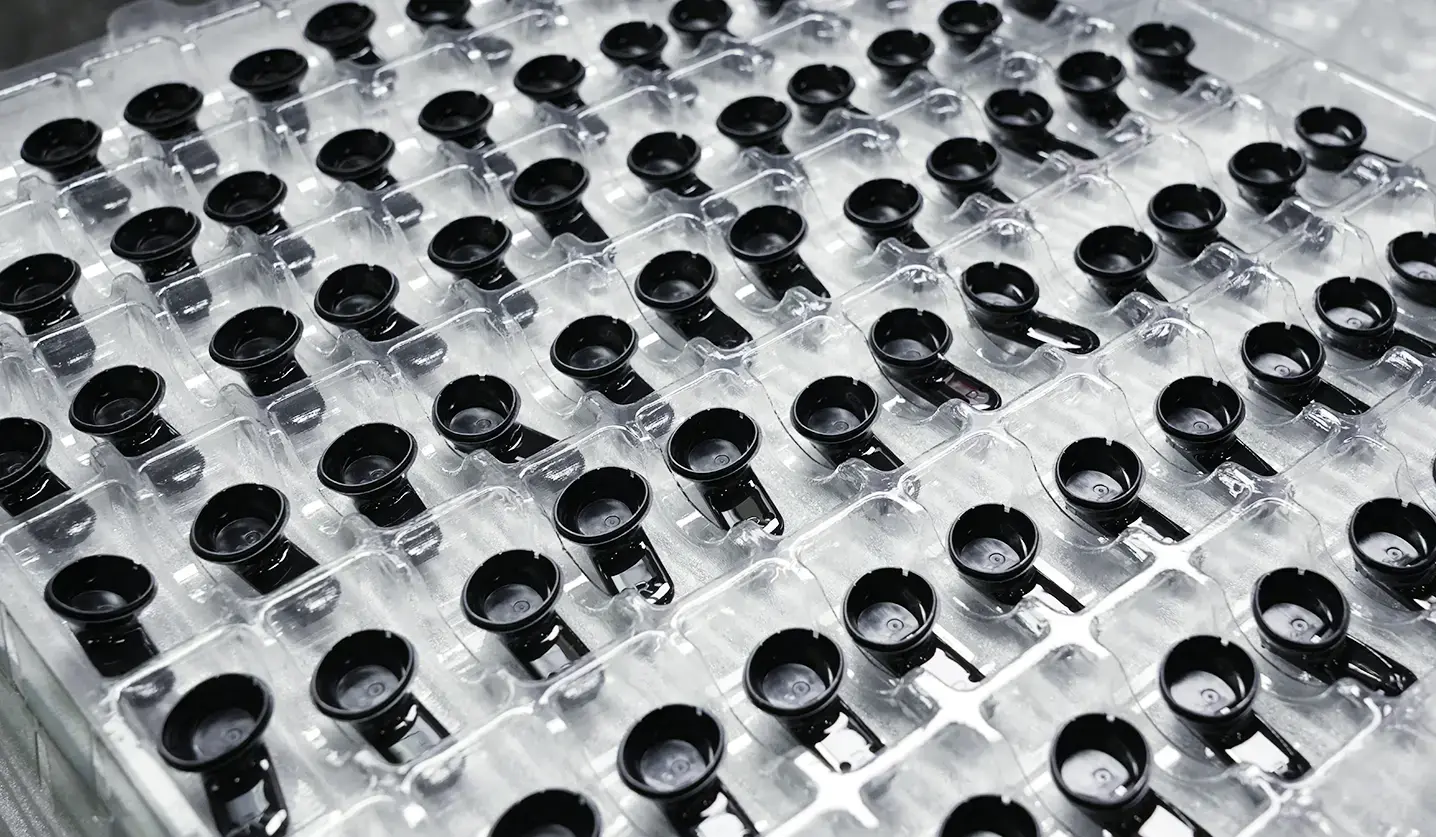
First Mold operates over 60 advanced injection molding machines. Our parameters can support the vast majority of part production projects.
50 +
تصنيع القوالب الشهرية
± 0.005 مم
Tooling Tolerance
| المواصفات | المعلمات | المواصفات | المعلمات |
|---|---|---|---|
| الحمولة الإجمالية للآلة | 90T – 1000T (60+ Sets) | القدرة الإنتاجية | >45,000,000 قطعة/سنة (>3.5 مليون/شهر) |
| الأبعاد القصوى (الطول × العرض × الارتفاع) | 1500 × 1000 × 500 ملم | الأبعاد الدنيا | 5 × 5 × 5 ملم |
| Parts Standard Tolerance | ±0.1 مم (±0.004 بوصة) | Parts Precision Tolerance | ±0.05 مم (±0.002 بوصة) |
| مهلة التصنيع السريع للأدوات السريعة | 7 – 15 Days | أدوات الإنتاج | 3 – 10 weeks (Automotive: 45 Days) |
| معيار الجودة | DIN-7168-m / ISO 2768-m | Inspection/QC | CMM, VMS, FAI Reports |
Scalable Plastic Injection Molding Process
We build the molds and manufacture your parts entirely in-house. There are no vendor handoffs, no re-engineeringو zero dimensional errors.
Rapid Prototyping & Short Runs
Get T1 production-grade physical parts in 7 to 15 days. We use rapid tooling and scientific molding to validate your design fast.
Low-Volume (Bridge Tooling)
If your demand grows, we can often upgrade your initial quick mold by replacing only the core parts while keeping the mold base.
High-Volume Mass Production
High-volume injection molding for production parts. Hardened steel tooling built for 1,000,000+ shots, with lower unit costs as volume scales.
Advanced Molding Capabilities
100+ Plastic Materials for Injection Molding
We mold over 100 commercial and engineering-grade resins every year. Our injection molding process accommodates custom Pantone color matching, UV stabilizers, and up to 50% glass fiber (GF) reinforcement for enhanced strength.
| الدرجات المشتركة | Standard, PC/ABS Blend, Flame Retardant (UL94-V0) |
| Key Specs | Shrinkage 0.4%-0.7% | HDT ~85°C |
| Typical parts | Appliance housings, decorative trim |
| الدرجات المشتركة | PA6, PA66, Glass-Filled (10%-50% GF), MoS2 Filled |
| Key Specs | Shrinkage 1.0%-1.5% | HDT Up to 250°C (with GF) |
| Typical parts | Cable ties, automotive connector housings |
| الدرجات المشتركة | Optically Clear, UV Stabilized, Glass-Reinforced |
| Key Specs | Shrinkage 0.5%-0.7% | HDT ~135°C |
| Typical parts | Safety guards, helmet shells |
| الدرجات المشتركة | Standard, 30% GF, Flame Retardant (V-0) |
| Key Specs | Shrinkage 1.5%-2.0% | HDT Up to 210°C (with GF) |
| Typical parts | Electrical connectors, sensor housings |
| الدرجات المشتركة | Unfilled, 30% Glass-Filled, Carbon Fiber-Filled |
| Key Specs | Shrinkage 1.0%-1.5% | HDT Up to 315°C (with CF) |
| Typical parts | Medical implant components, high-temperature fixture insulators |
| الدرجات المشتركة | Standard Clear, Impact-Modified, UV-Resistant |
| Key Specs | Shrinkage 0.2%-0.8% | HDT ~95°C |
| Typical parts | Light guides, indicator lenses |
Surface Finishes & Secondary Operations
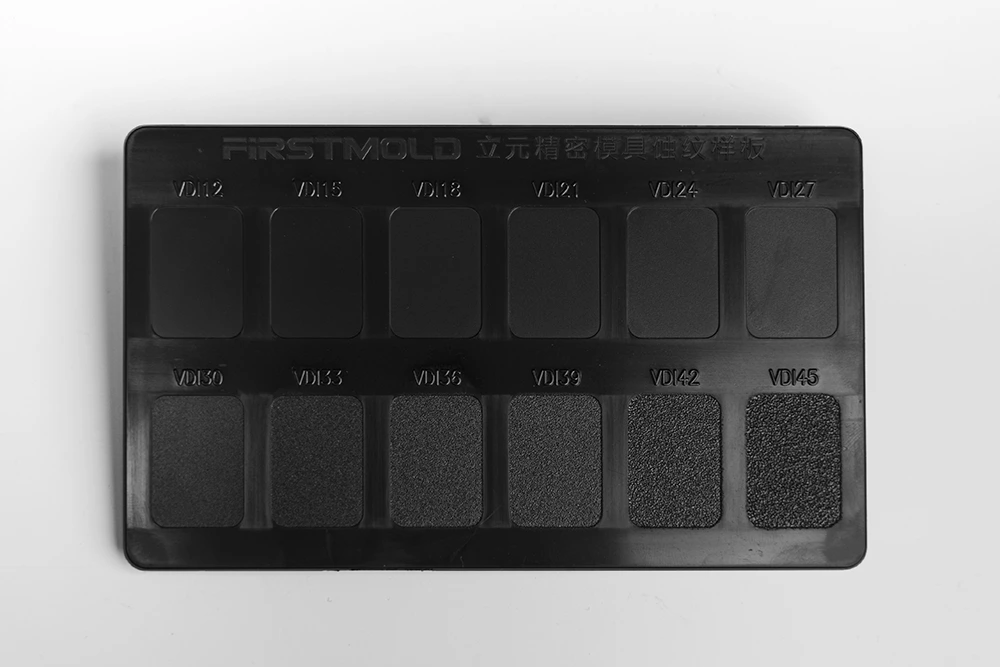
The mold shapes the part; the finish defines how it looks, feels, and performs. From in-mold SPI/VDI textures to advanced post-molding operations, we provide end-to-end finishing services to turn raw molded parts into production-ready components.
التشطيبات داخل القالب
| قياسي | فئة النهاية | الخشونة Ra (ميكرومتر) |
|---|---|---|
| SPI A1 – A3 | صقل الماس / لمعان عالي | 0.012 – 0.10 |
| SPI B1 – B3 | ورق صنفرة / شبه لامع | 0.05 – 0.32 |
| SPI C1 – C3 | تشطيب حجري / أملس غير لامع | 0.35 – 0.7 |
| SPI D1 – D3 | التنظيف بالرمل / المزخرف | 0.80 – 18.0 |
| VDI 3400 (12-45) | EDM / نسيج ناتج عن التآكل بالشرر الكهربائي | 0.40 – 18.0 |
هل تحتاج إلى مساعدة في تحديد الشكل النهائي التجميلي أو الوظيفي الدقيق لقطعتك؟ لا تتردد في التواصل مباشرةً استشر مهندسي DFM لدينا للحصول على توصيات خاصة بالمشروع.
العمليات الثانوية
Coatings & Metallization
الطلاء الكهربائي
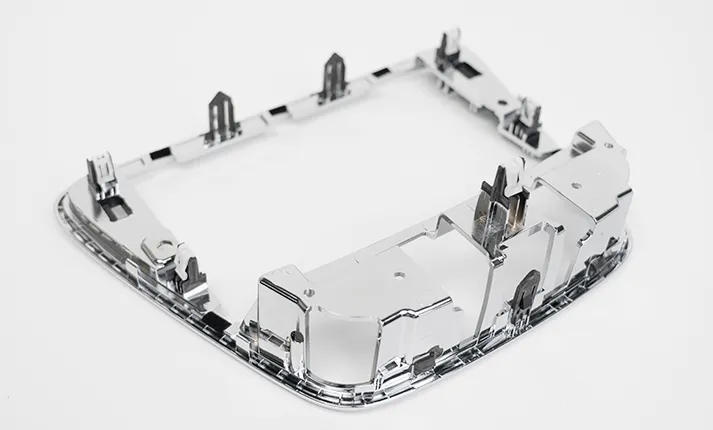
يمنح البلاستيك الخفيف الوزن المظهر نفسه والملمس البارد والمقاومة الفائقة للتآكل التي يتميز بها المعدن الصلب.
PVD
يمنحك لمسة نهائية معدنية لامعة ومقاومة للخدش تشبه المرآة.
Branding & Decoration
الطباعة
Pad printing, silk screening, and hot stamping for multi-color graphics and warnings.
Surface Machining
الطحن والتلميع
يزيل تمامًا آثار بوابات الحقن وخطوط الفصل ليمنح ملمسًا ناعمًا تمامًا
كيف نضمن خلو قطعك البلاستيكية من العيوب تمامًا؟
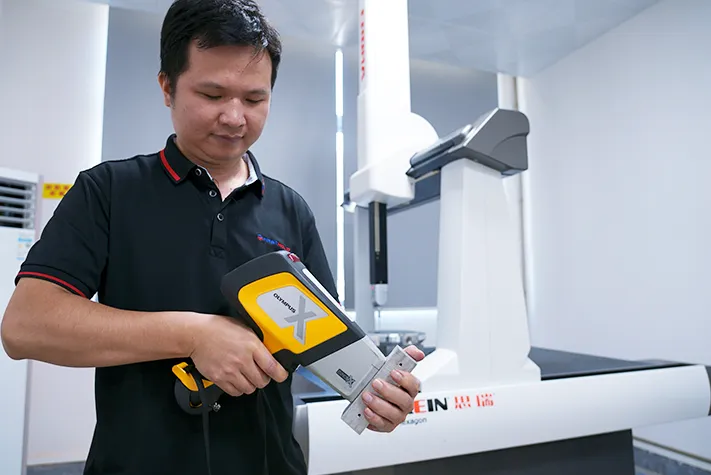
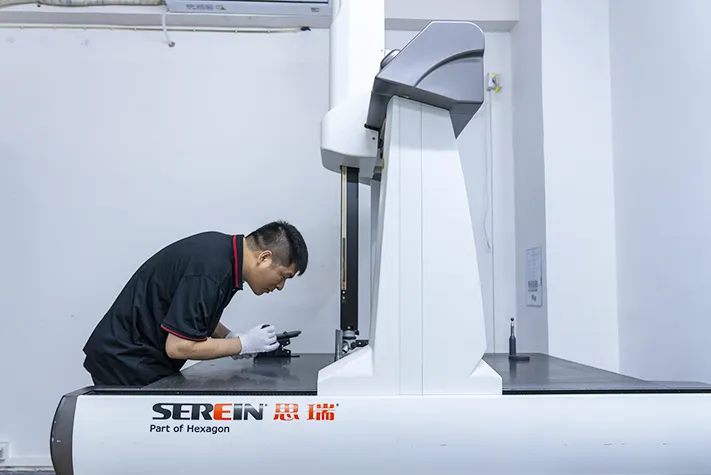
We rely on metrology and statistical process control (SPC), not guesswork. First Mold inspects and corrects critical parameters across multiple production stages.
| QA Stage | أساليبنا ومعداتنا | نقاط الفحص الرئيسية |
|---|---|---|
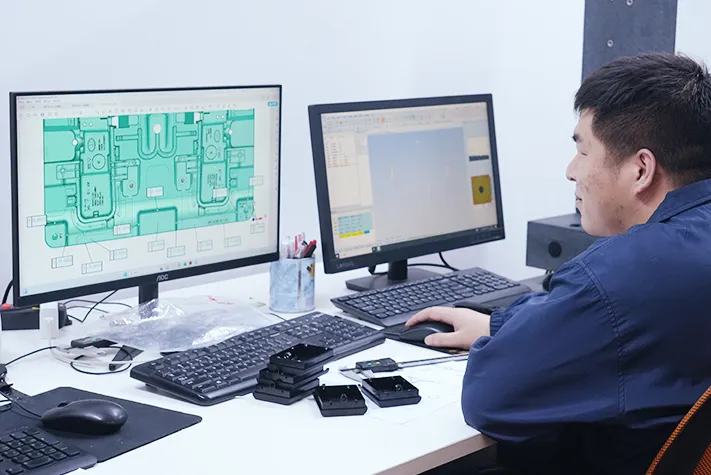
| 1. مرحلة ما قبل الإنتاج | مراجعة التصميم من أجل التصنيع (DFM) وتحليل تدفق القالب | زوايا التصميم، وتوحيد سماكة الجدران، ومواقع فتحات الصب، وخطوط اللحام، وعلامات الانغماس، وتوقع الالتواء، ومعدلات الانكماش، والتجاويف السفلية، وتصميم قنوات التبريد، واستراتيجيات التهوية. |
| 2. الأدوات والإعدادات | First-article Inspection (FAI) & T1 Sampling | دقة الأبعاد، مطابقة نماذج CAD ثلاثية الأبعاد، التحقق من المواد، جودة تشطيب السطح، ملاءمة التجميع، كشف الحواف الزائدة، عدم تطابق خط الفصل، نقص في حقن البلاستيك، علامات دبابيس الإخراج. |
| 3. قيد التصنيع والنهائية | CMM & 2d Vision Measurement | التفاوتات الحرجة، الأشكال الهندسية المعقدة، gd&t (الأبعاد الهندسية والتفاوتات)، الاستواء، التراكز، أقطار الثقوب، انحرافات المقطع الجانبي، الموضع الحقيقي، العموديّة. |
| 4. النظام والامتثال | البروتوكولات الحاصلة على شهادة ISO والتتبع | تتبع المواد، الاتساق بين الدفعات، تنفيذ إجراءات التشغيل القياسية، تقارير مراقبة الجودة، شهادة تحليل الراتنج (COA)، الحد من العيوب، سجلات صيانة الأدوات. |
Industry-Specific Molding Solutions & Case Studies
A closer look at how we solve complex manufacturing challenges across automotive, medical, consumer electronics, and industrial sectors using tailored resins and strict process controls.
| الصناعة | Engineering Focus | Featured Projects (Click to read case studies) |
| السيارات | Metal-to-plastic conversion, high-temp resistance, structural rigidity. | [Gearbox Cover], [Sensor Housing], [Dashboard Bracket], [Ignition Coil Shell] |
| الطبية | Biocompatibility, tight tolerances (±0.02mm), sterilization ready. | [Surgical Tool Handle], [Ventilator Enclosure], [Dialysis Machine Valve] |
| الإلكترونيات الاستهلاكية | Thin-wall molding, SPI A2 high gloss finish, EMI shielding. | [Drone Outer Shell], [Smartwatch Bezel], [Router Housing], [VR Headset Frame] |
| Industrial | High impact resistance, wear reduction, thick-wall anti-sink. | [Conveyor Gear], [Pump Impeller], [Heavy-Duty Pulley], [Motor Housing] |
| Home Appliance | Complex assembly reduction, cosmetic surface consistency. | [Smart Thermostat Cover], [Blender Base], [Air Purifier Grille] |
Our Plastic Injection Molding Workflow at First Mold
We don’t treat your CAD files as a black box. At First Mold, our plastic injection molding process is completely transparent. Here is the exact step-by-step roadmap.
Submit CAD for Engineering Review
Upload your 3D models (STEP/IGES/X_T). Our engineers analyze your geometry and provide an itemized plastic injection molding quote and initial feasibility feedback within 24 hours.
DFM Approval & Mold Fabrication
Review our comprehensive DFM report detailing draft angles, shrink rates, and gating strategies. Upon your sign-off, we immediately begin CNC machining and cutting steel for your custom mold.
T1 Sampling & FAI Verification
We shoot the first physical plastics from your mold. You receive these T1 off-tool samples alongside a complete First Article Inspection (FAI) dimensional report for your engineering validation.
Mass Production & Global Logistics
Once you approve the T1 samples, we lock in the molding parameters for full-scale production. First Mold manages strict SPC quality control, packaging, and direct global shipping to your facility.
Tips: New to our quoting system? Watch this quick 3-minute demo to see exactly how to submit your CAD and get pricing: How to Get a Part Production Quote from First Mold
Recommended Structural Design Guidelines for Injection Molding
Our engineers highly recommend applying these proven structural parameters to your CAD models to avoid costly mold modifications and achieve flawless parts on the first shot.
- Maintain a uniform thickness (1.5–3.0mm). Keep variations under 20% to prevent sink marks and uneven cooling shrinkage.
- Design internal ribs at 50%–60% of the adjacent outer wall's thickness to prevent visible sink marks on the exterior.
- Avoid sharp internal corners. Add a 0.3–0.5mm minimum radius to reduce stress, prevent cracking, and improve melt flow.
- Apply 0.5°–2° draft on vertical walls. Make the cavity draft 0.5° larger than the core to keep the part on the core during ejection.
- Locate parting lines on the part's maximum contour. Avoid high-gloss or critical assembly surfaces to minimize visible flashing.
- Design text and logos as raised (embossed). Machining recessed text into the mold steel is significantly easier and cheaper than machining raised letters.
- Limit blind hole depth to 3 times the diameter. Deeper holes risk bending or breaking core pins under high injection pressure.
- Do not attach thick bosses directly to main walls. Use connecting ribs and a coring base ("volcano") to prevent exterior sink marks.
- Keep metal inserts ≥5mm from the cavity wall. Preheat them to 80–120°C before molding to prevent thermal stress cracking during shrinkage.
- Add a 0.2–1.0mm cosmetic groove (reveal) at mating lines to seamlessly hide inevitable molding tolerances and mismatch.
- Design mating lips with 0.8–2.5mm depth and 0.1mm side clearance. Keep vertical top and bottom faces at zero gap for a stable fit.
- For reliable assembly, use 1.0–1.5mm cantilever thickness, length under 8x the thickness, and 0.3–0.5mm hook depth.
Plastic Injection Molding FAQ